
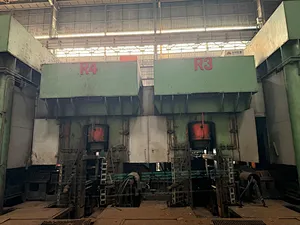

700mm HRM
1. Production Scale and Products
Annual Production Capacity: 1.5 million tons of strip steel coils.
Product Specifications:
Thickness: 1.0 - 7.0 mm
Width: 315 - 520 mm
Max Coil Weight: 6 tons
Max Coil Outer Diameter: Φ1600 mm
Steel Grades: Ordinary carbon steel, high-quality carbon structural steel, low-alloy steel, etc.
Product Standards: Complies with various Chinese national standards (GB) for hot-rolled strip, including GB/T8164, GB709, and GB710.
2. Raw Materials
Raw Material Type: 100% Continuous casting slabs.
Billet Specifications:
Thickness: 150 mm
Width: 330 - 520 mm
Length: 9000 - 10000 mm
Max Weight: 6 tons
3. Main Process Flow
Slab Heating: Slabs are heated to approximately 1250°C in a walking beam furnace.
Descaling: A high-pressure water descaling unit removes the primary oxide scale from the heated slab surface.
Roughing Rolling: The scaled slab is rolled in an 8-stand roughing mill (arrangement: 1 Vertical, 2 Horizontal, 1 Vertical, 2 Horizontal, 1 Vertical, 1 Horizontal) into an intermediate strip with a thickness of 28–35mm.
Crop Shearing: A flying shear crops the head of the intermediate strip to facilitate entry into the finishing mill.
Finishing Rolling: The intermediate strip is rolled to the final thickness in a 10-stand finishing mill (1 Vertical, 9 Horizontal). A secondary descaling unit is located after the first finishing stand (E4) to remove secondary scale.
Cooling and Coiling: The finished strip is cooled on a flat chain conveyor and then coiled by a vertical, shrink-core-type coiler. The coils are then transferred to a conveyor chain for final handling and storage.
4. Core Technical Features
Fully Continuous Layout: Features a continuous setup with"off-head"rolling between the roughing and finishing mills for high production efficiency.
High-Precision Control Systems:
Gauge Control: All F1-F9 finishing stands are equipped with hydraulic AGC (Automatic Gauge Control) for precise thickness control.
Width Control: The E1-E4 vertical edgers utilize hydraulic AWC (Automatic Width Control) and SSC (Short Stroke Control) for superior width accuracy.
Tension Control: Eight low-inertia electric loopers between the finishing stands ensure constant micro-tension rolling for improved shape and dimensional stability.
Advanced Instrumentation: The line is equipped with imported thickness gauges and width gauges after the finishing mill for real-time monitoring and control of product quality.
Temperature Management: Insulation covers between the roughing and finishing mills minimize temperature loss of the intermediate strip. The final rolling temperature is controlled between 850°C and 950°C.
Efficient Coiling: A robust vertical, shrink-core-type coiler handles strip at speeds up to 15 m/s, with a maximum coil weight of 6 tons.
Drive and Lubrication: Main mill stands are driven by DC motors. The roll systems and bearings use advanced oil-air lubrication for reliability and longevity.
5. Main Equipment Composition
Roughing Mill Unit:
E1-E3 Vertical Edgers: Hydraulic AWC+SSC control. Roll size: Φ650/600x400mm.
R1-R5 Two-High Horizontal Mills: Hydraulic APC (Automatic Position Control) screw-down. Roll size: Φ690/630x670mm.
Finishing Mill Unit:
E4 Vertical Edger: Hydraulic AWC+SSC control. Roll size: Φ600/550x200mm.
F1-F2 Two-High Mills: Hydraulic AGC. Work Roll size: Φ660/610x670mm.
F3-F9 Four-High Mills: Hydraulic AGC. Work Roll size: Φ360/400x700mm; Backup Roll size: Φ660/610x670mm.
Shearing Equipment:
Rotary Drum Flying Shear: Located before the finishing mill for head cropping. Max shear force: 2500 KN.
Coiling Equipment:
Vertical Colier: Shrink-core type with a φ520/500mm core.


